Why Use an Emulsifying Solubilizer in Formulations?
Why Use an Emulsifying Solubilizer in Formulations?
Modern personal-care products must combine ingredients that naturally resist each other. Oil, water, fragrances, and active compounds often separate without careful formulation. An Emulsifying Solubilizer helps disperse oil-soluble materials through aqueous systems. It can improve clarity, texture, stability, and consumer acceptance. The result may be a uniform facial mist, a smooth lotion, or a transparent cleansing gel.
The market evidence is substantial. Grand View Research valued the global cosmetics market at approximately USD 446.2 billion in 2023. It also forecasts continued growth through 2030. Cosmetics Europe reported European cosmetics and personal-care retail sales of about EUR 104 billion in 2023. These figures reflect stronger demand for convenient, stable, and pleasant products. They do not prove that one ingredient guarantees success. That assumption is tempting, but incomplete.
A well-selected Emulsifying Solubilizer can reduce visible oil droplets, support fragrance incorporation, and improve formula consistency during storage. It may also reduce processing difficulties, especially when manufacturers work with limited heating or sensitive botanical extracts. However, performance depends on concentration, pH, electrolyte content, oil polarity, and processing energy. Small laboratory batches can look perfect, then separate after temperature cycling. That happens.
Technical evaluation should include centrifuge testing, freeze–thaw cycles, accelerated aging, viscosity measurement, and microbial-control checks. Suppliers’ technical dossiers, safety data, and compatibility studies strengthen decision-making. Formulators should also confirm regulatory suitability in each target market. No single solubilizer fits every application. The best choice balances stability, sensory feel, transparency, cost, and the final product’s use conditions. Industry reports show market momentum, but disciplined testing creates reliable formulations.
Emulsifying Solubilizers Explained: The HLB Scale from 0 to 20
Why Use an Emulsifying Solubilizer in Formulations?
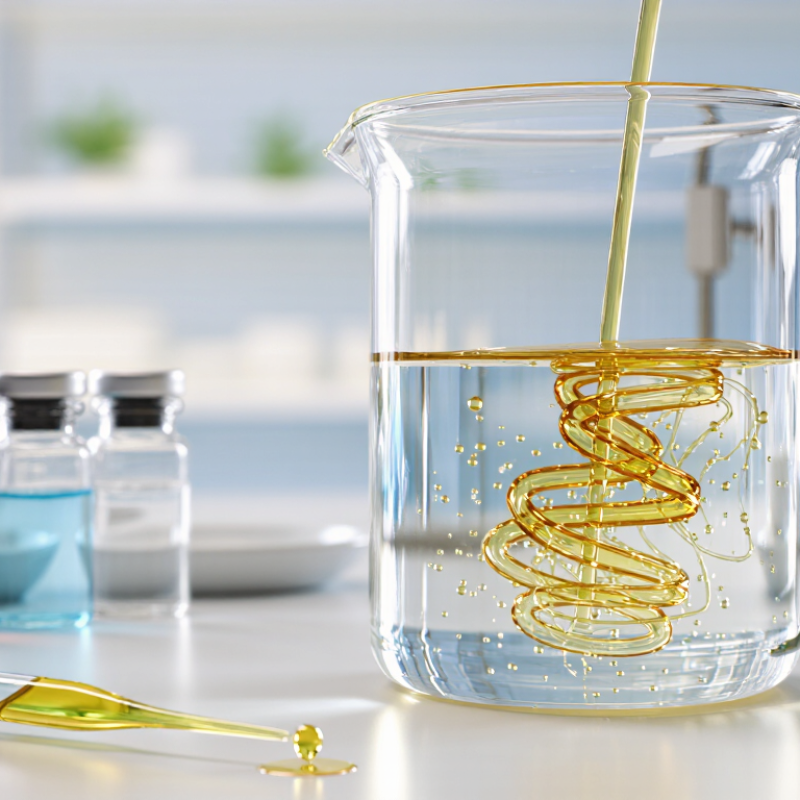
The HLB scale helps formulators choose an emulsifying solubilizer more logically. HLB means hydrophilic-lipophilic balance. It usually ranges from 0 to 20. Lower values indicate stronger oil affinity. Higher values indicate stronger water affinity. Materials near 3 to 6 often support water-in-oil systems. Values around 8 to 18 generally suit oil-in-water systems or solubilization. These ranges are useful guides, not fixed laws.
In practical development, I first identify the oil phase and its required HLB value. A lightweight fragrance oil may need a different balance from a waxy botanical extract. A higher-HLB solubilizer can help disperse a few drops of oil into a clear water base. However, clarity may change after heating, cooling, or adding electrolytes. The scale is not a verdict. That shortcut failed.
Small bench trials reveal more than a calculation alone. I prepare several samples with different solubilizer ratios, then observe them after 24 hours and one week. I check cloudiness, separation, viscosity, odor, and skin feel. pH can also influence performance. Mixing speed matters, too. A formula may look stable immediately but develop a floating ring later. Careful records improve repeatability and support reliable decisions.
Selecting Dosage and HLB Balance: Typical Use Levels of 0.5%–5%
An emulsifying solubilizer helps disperse small amounts of oil in water-based formulations. Its dosage strongly affects clarity, stability, texture, and skin feel. Typical use levels range from 0.5% to 5%, but the right amount depends on the oil load and solubilizer type.
A practical starting point is 1% solubilizer for a light fragrance or essential oil phase. Increase gradually when cloudiness, separation, or surface oil appears. For heavier oils, 2%–5% may be necessary. More is not always better. Excess solubilizer can create stickiness, foam, or an unpleasant drag during application. Small bench trials reveal these changes quickly.
HLB balance also matters. The required HLB of the oil phase should guide ingredient selection and dosage. A mismatch may produce temporary clarity but poor long-term stability. Check samples after heating, cooling, shaking, and several weeks of storage. pH and electrolytes can change performance unexpectedly. Clear today?
Record every adjustment, including mixing speed and addition order. In practical formulation work, these details often explain inconsistent results. A useful method is testing 0.5%, 1%, 2%, and 5% in parallel. Compare appearance, viscosity, odor release, and separation. The best level is usually the lowest one that remains stable under realistic conditions. Yet this approach is not perfect; some systems need longer observation than a quick laboratory screen.
Enhancing Formula Stability Through 40°C/75% RH Accelerated Testing
Why Use an Emulsifying Solubilizer in Formulations?
Enhancing Formula Stability Through 40°C/75% RH Accelerated Testing
An emulsifying solubilizer helps disperse oil-soluble materials through an aqueous formula. It can strengthen the interfacial film between oil and water. This matters during accelerated stability testing. Under ICH Q1A(R2), samples are commonly held at 40°C ± 2°C and 75% ± 5% relative humidity for six months. Heat speeds molecular movement, while humidity challenges packaging and product consistency. A weak system may show creaming, separation, odor changes, or viscosity loss within weeks. A well-selected solubilizer can delay these failures, but it cannot repair poor processing or incompatible ingredients.
Practical screening should compare several solubilizer levels, mixing speeds, and addition temperatures. Record appearance, pH, viscosity, particle size, and centrifugation results. ISO/TR 18811:2018 also emphasizes that cosmetic stability protocols should reflect the product and packaging, rather than follow one universal recipe. That is easy to overlook. In my lab experience, clear samples can still develop hidden oxidation or fragrance loss. Visual inspection alone is not enough.
Tips: Use small pilot batches first. Test the formula in its final container. Inspect at 0, 2, 4, and 8 weeks. Include room-temperature controls. Review every change against ICH Q1A(R2) and ISO/TR 18811:2018. Do not assume higher solubilizer levels always improve stability; excess material may reduce sensory quality or increase irritation potential.
Why Use an Emulsifying Solubilizer in Formulations? - Enhancing Formula Stability Through 40°C/75% RH Accelerated Testing
Representative, non-brand comparative screening dataset. Values should be confirmed using the final formula, packaging, manufacturing process, and validated analytical methods.
| Test Dimension |
Control Formula
(Without Solubilizer) |
Formula A
(Low Solubilizer Level) |
Formula B
(Optimized Solubilizer Level) |
Typical Evaluation Target |
| Oil phase |
3.0% w/w |
3.0% w/w |
3.0% w/w |
Constant across batches |
| Emulsifying solubilizer |
0.0% w/w |
0.75% w/w |
1.50% w/w |
Optimize for clarity, feel, and stability |
| Initial appearance |
Slightly hazy |
Opalescent |
Uniform and translucent |
No visible oil droplets or sediment |
| Initial pH at 25°C |
5.42 |
5.40 |
5.41 |
Product-specific target, typically ±0.30 pH units |
| Initial viscosity at 25°C |
410 mPa·s |
430 mPa·s |
445 mPa·s |
Change generally within ±20% |
| Initial mean droplet size, D50 |
1.80 µm |
1.10 µm |
0.72 µm |
Smaller and more uniform droplets generally improve physical stability |
| 40°C / 75% RH exposure |
Accelerated condition |
Accelerated condition |
Accelerated condition |
Common long-term accelerated storage condition for stability screening |
| Appearance after 4 weeks |
Visible creaming; slight separation |
Mild increase in haze |
No visible separation |
No phase separation, precipitation, or unacceptable color change |
| pH after 4 weeks |
5.08 |
5.22 |
5.31 |
Change from initial value not more than 0.30 units |
| Viscosity after 4 weeks |
305 mPa·s |
375 mPa·s |
420 mPa·s |
Change generally within ±20% of initial value |
| Mean droplet size after 4 weeks, D50 |
3.40 µm |
1.65 µm |
0.98 µm |
Limited droplet growth during storage |
| Centrifuge stress test |
Separation observed at 3,000 × g for 30 min |
Trace creaming |
No visible separation |
No visible separation after defined stress cycle |
| Freeze–thaw cycles |
2 of 3 cycles failed |
1 of 3 cycles failed |
0 of 3 cycles failed |
No irreversible separation or precipitation |
| Overall screening outcome |
Needs reformulation |
Partially acceptable |
Best-performing prototype |
Confirm with full stability and compatibility studies |
Testing note:
Accelerated storage at 40°C and 75% relative humidity can reveal creaming, coalescence, viscosity drift, pH change, precipitation, and packaging-related instability more quickly than ambient storage. Solubilizer concentration should be optimized because excessive surfactant may affect skin feel, foam, irritation potential, and preservative performance.